
Why manufacturers keep stumbling on catheters
You’re trying to move from concept to reliable production and the same problems keep popping up: inconsistent wall thickness, coatings that delaminate, parts that don’t meet torque or pushability specs. Those are the day-to-day headaches when you work on interventional medical devices, and they cost time, reputation, and budgets if you don’t fix them early.
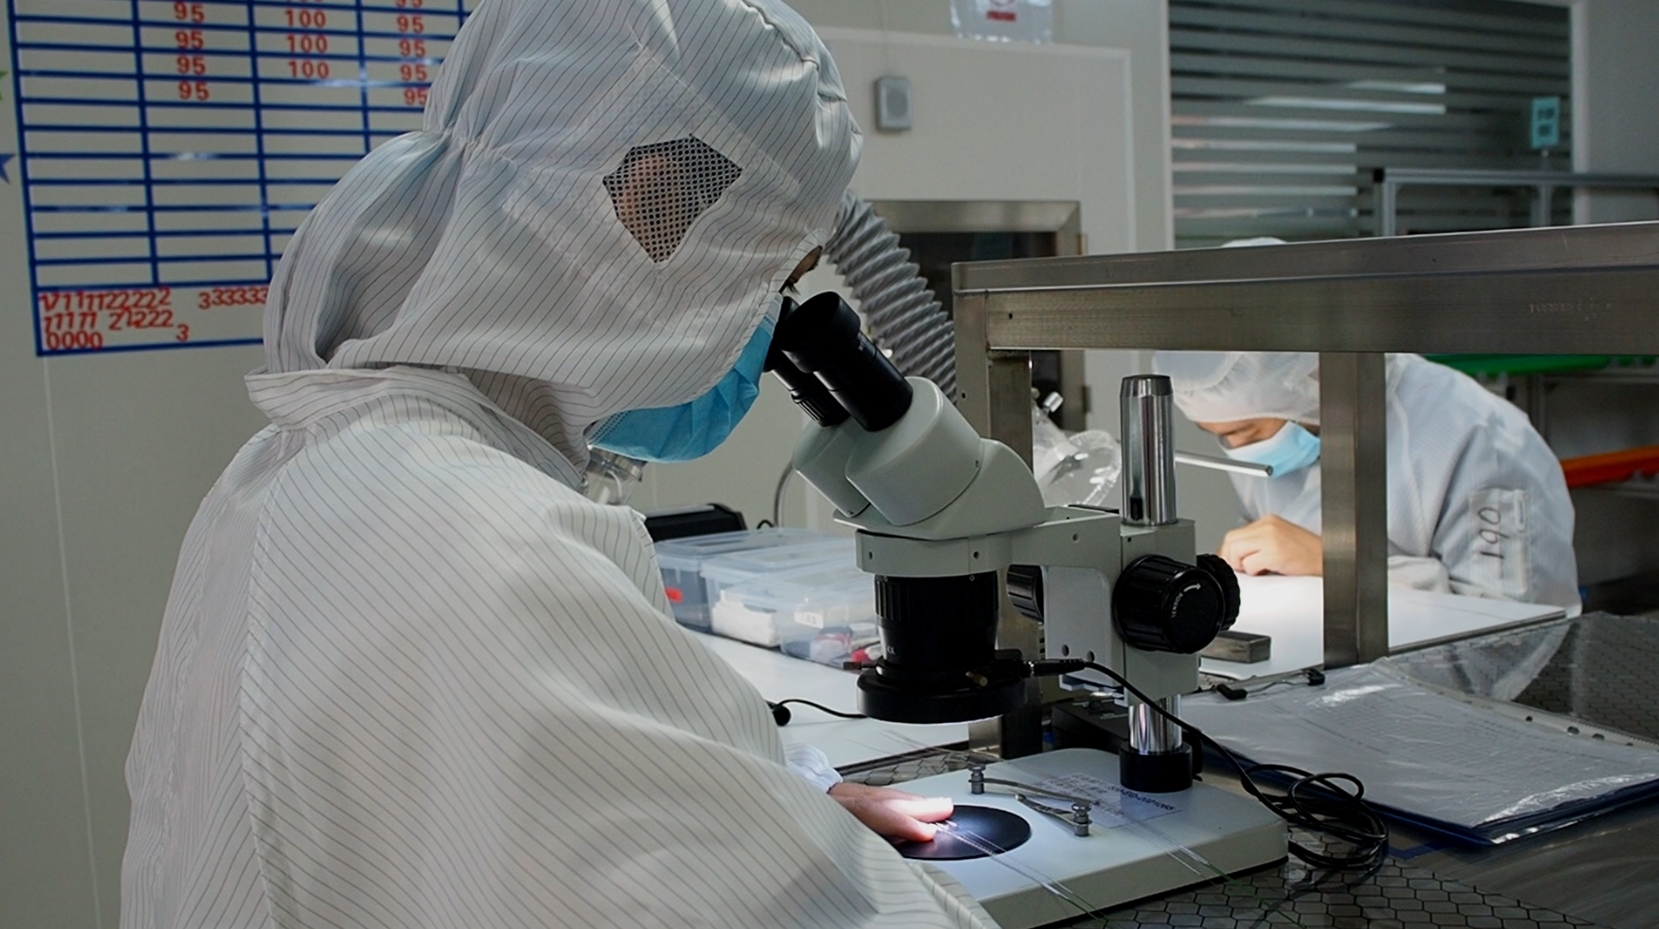
Top production problems that actually stop launches
Unexpected variability in extrusion tolerances wrecks handling. Poor bonding between shafts, tips, and radiopaque markers causes failure during use. Hydrophilic coatings can behave great in a lab but wash off in practice. Sterilization—especially ETO or gamma—changes materials in ways engineers often miss. Supply-chain gaps for specialty polymers or braiding wire create sudden delays. These are the exact bottlenecks you’ll hit if specs aren’t bulletproof and process controls aren’t tight.
Design and materials: specific controls that matter
Call out measurable targets: shaft ID/OD tolerances in microns, burst pressure, kink radius, torque response, and coating adhesion tests. Use materials with proven biocompatibility—PTFE liners for low friction, polyether block amide or Pebax blends for shaft flexibility, and platinum-iridium markers for visibility under fluoroscopy. Specify assembly joins (thermal bond vs. adhesive) and validate them with pull and cyclic fatigue tests. Prototype early, then move straight into process capability studies so you’re not surprised when volumes scale up.
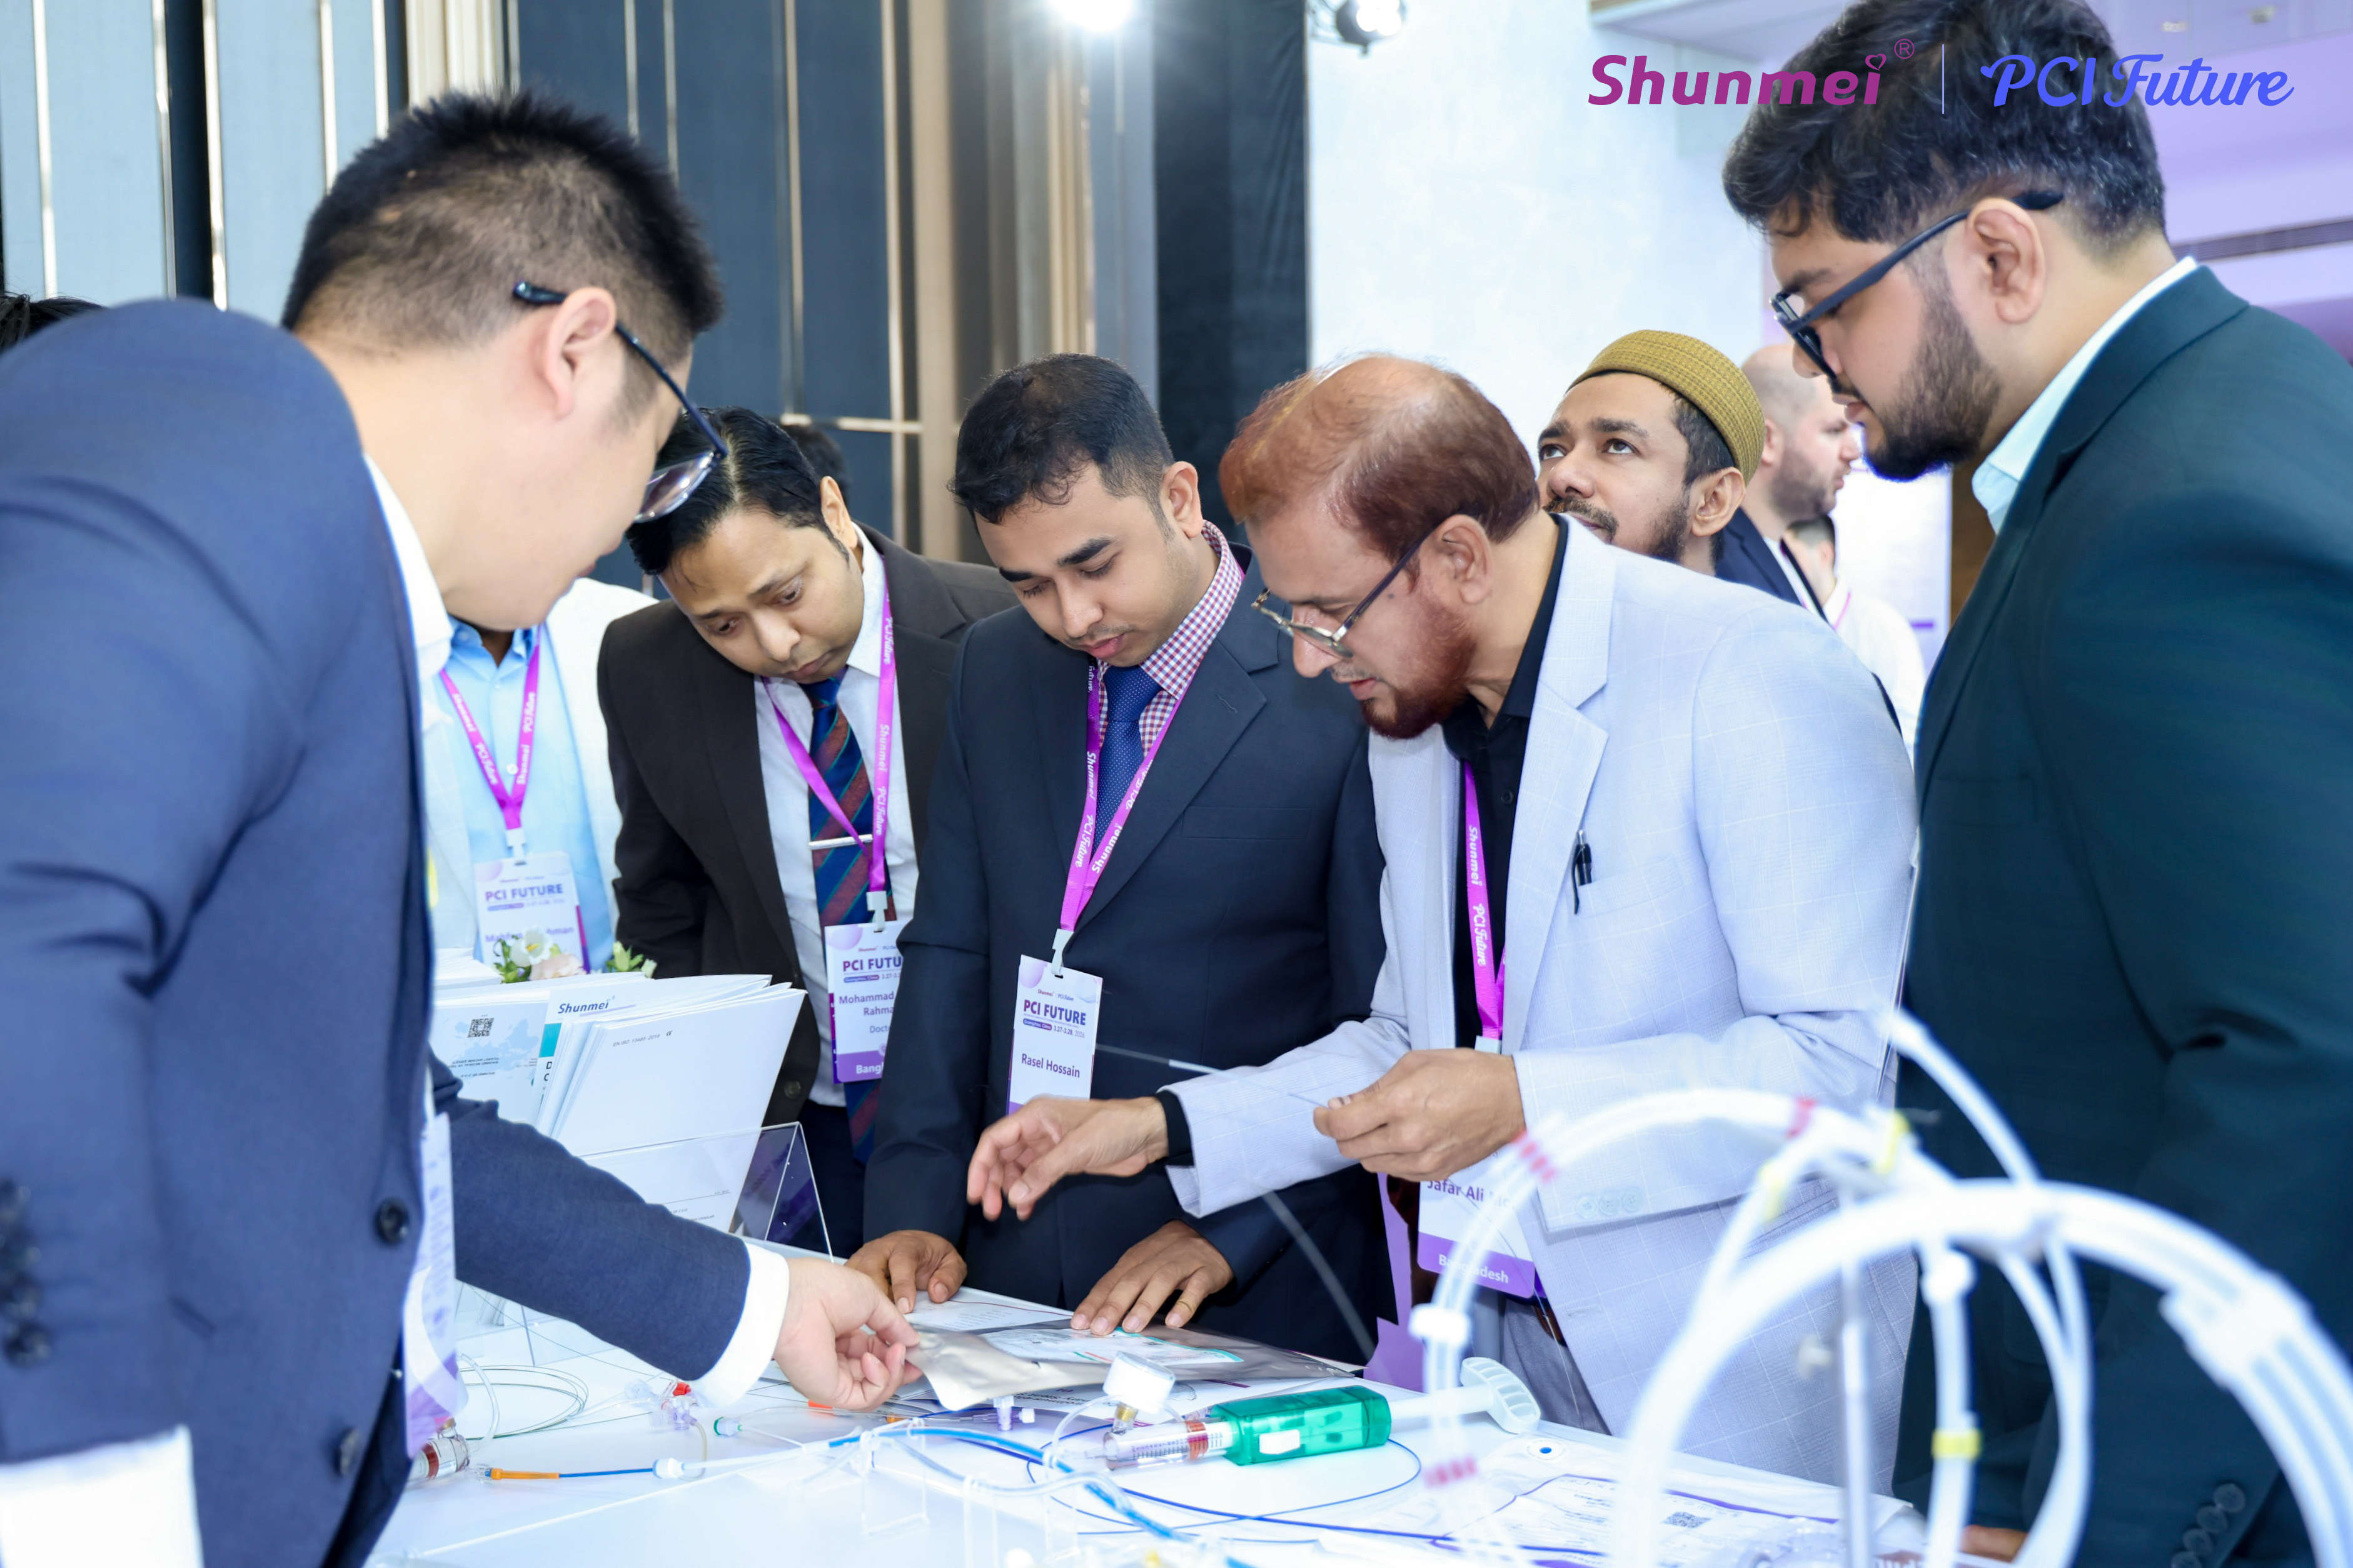
Experience, standards and a real-world anchor you can trust
Teams that ship reliable catheters pair hands-on device build experience with documented systems: ISO 13485-certified quality management, design history files, and FDA registration when applicable. Practitioners who attend major industry gatherings like the TCT annual meeting often point to clinical feedback as the decisive test of manufacturability. When you compare vendors, look for finished-device validation, lot release criteria, and published performance data for similar products—this is how suppliers show they can deliver real clinical outcomes. Also check partners that publicly list their work on interventional cardiology products so you can map their experience to your device needs.
Common pitfalls and realistic alternatives
Don’t under-specify requirements or assume a prototype equals production. Mistakes include leaving sterilization method undefined, skipping process validation for coatings, and not planning for long-lead specialty materials. Alternatives: keep production in-house for IP control but expect higher capital and longer time-to-market; pick a contract manufacturer for speed and expertise but vet their cleanroom class, sterile processing, and emergency capacity; choose a nearshore partner to balance oversight and cost. Evaluate tradeoffs with hard metrics: defect rates, lead-time variability, and MOQ thresholds.
Choosing a partner without second-guessing later
Get detailed process maps, audit results, and sample testing under clinical-use conditions. Require capability demonstrations: extrusion SPC charts, coating adhesion tests, sterilization validation reports, and packaging integrity after transport simulation. Ask for references from projects that reached clinical use. Teams that move faster focus on measurable guarantees rather than vague promises, and they prefer partners who share batch-level traceability and rigorous supplier controls—qualities you’ll find when you work with experienced OEMs like Shunmei that integrate design, materials know-how, and validated production into one workflow.